HYDAR
The ultimate autonomous, containerized bottled water production facility engineered for rapid response.
Deliver Safe Water at the Point of Need
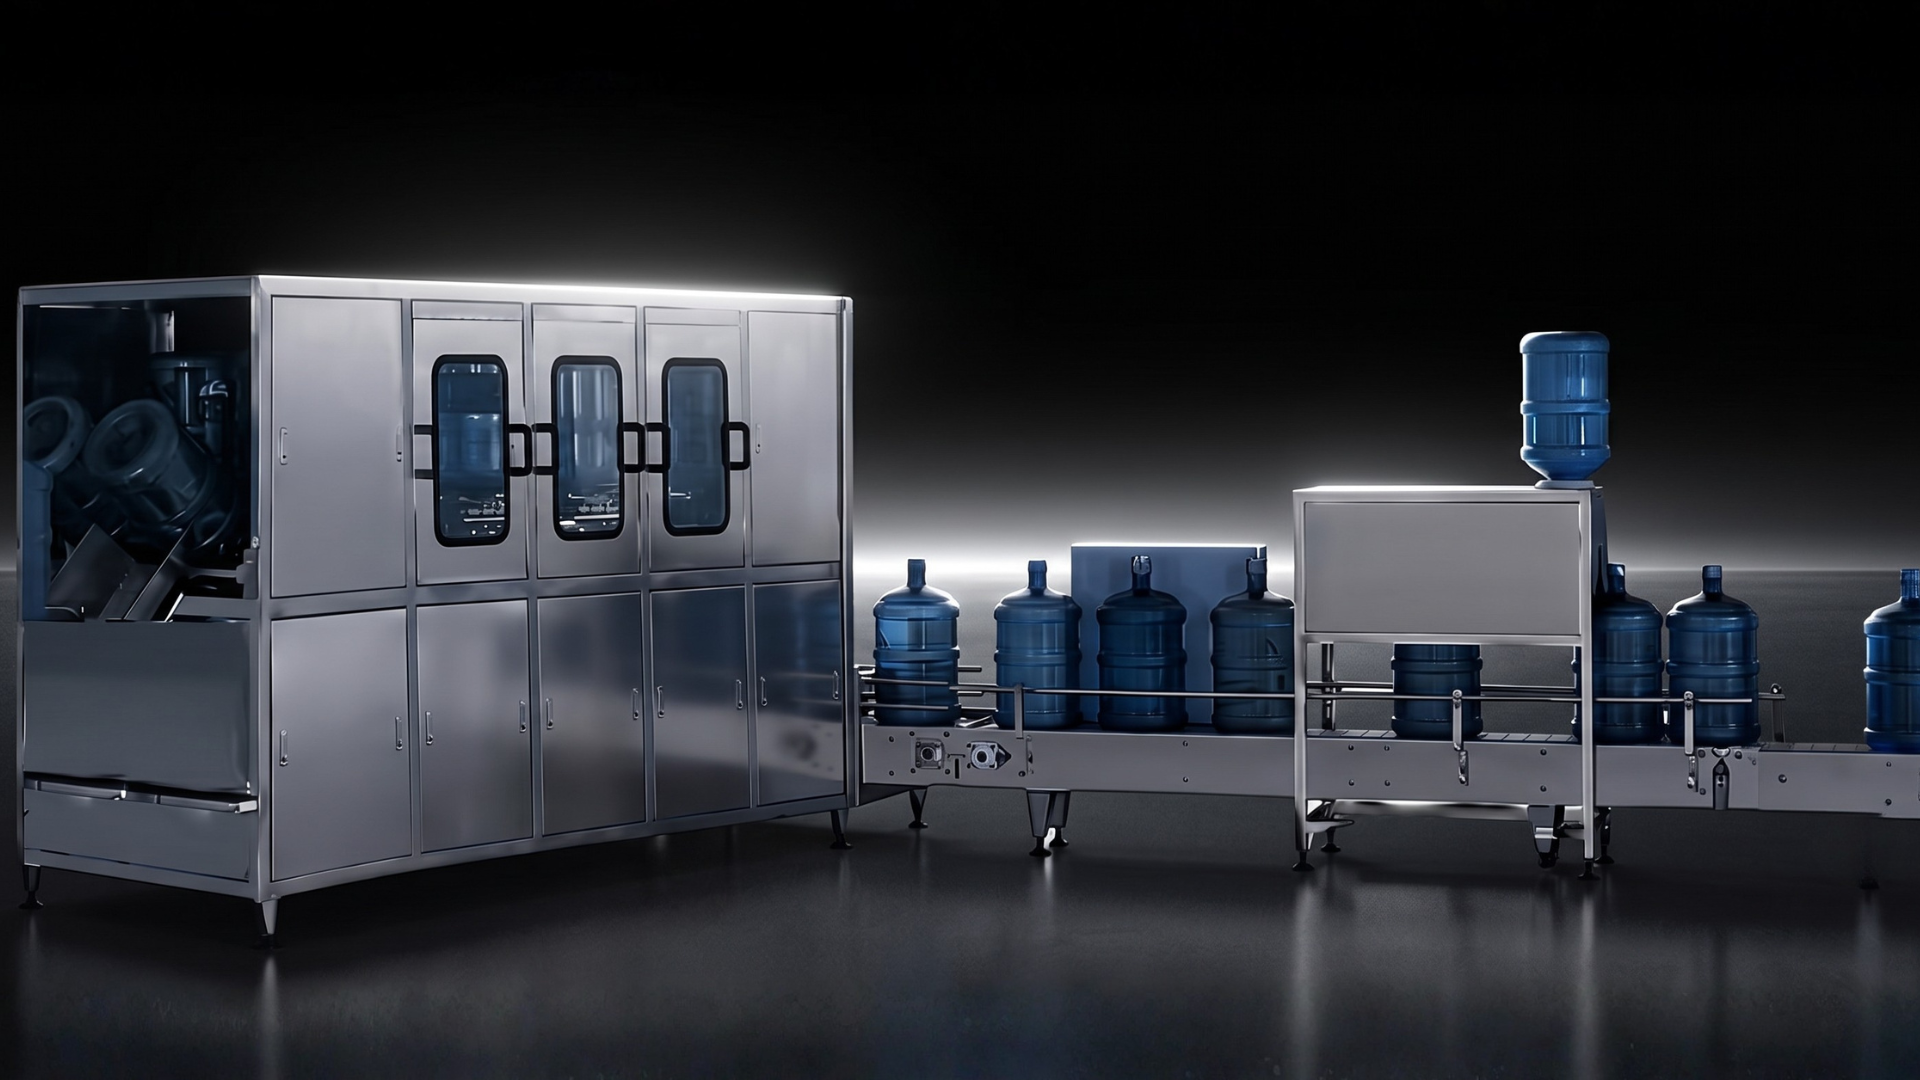
Complete, all-in-one automated water treatment and bottling facility housed inside a renovated, rapidly deployable shipping container.
High-Volume Processing
Specialized for producing standard 5-gallon (18.9L) PET bottles—the ultimate standard for sustained camp hydration.
Complete Sterilization
Features a 2m³/hour treatment system that includes Reverse Osmosis (RO), 5g Ozone sterilization, and dual 55W UV treatment to guarantee uncompromising water safety.
Rapid Workflow
An integrated, automated line handling everything from preform blow-molding to bucket brushing, automated internal washing, filling, capping, and shrink wrapping.
Compact & Efficient
Operates on a footprint of just 10 square meters with a total power requirement of 70 kW.
On-Site Bottle Blowing
Eliminates the need to ship empty bottles by blow-molding heavy-duty 18.9L bottles from preforms at 80 units per hour.
Rugged Deployment
The entire facility is housed in a reinforced, soundproofed, and insulated 40ft shipping container engineered for harsh environments.
A Complete Operational Workflow
Original Water Tank
Initial storage buffer optimizing inlet feed volume control.
Acts as the primary intake reservoir, stabilizing variable source flow rates before any treatment begins. Ensures consistent pressure and volume delivery to downstream filtration stages.
Quartz Sand & Activated Carbon
Dual-media filtration loop removing suspended solids, organic compounds, and chlorine.
Quartz sand captures macro-particulates while the activated carbon bed adsorbs chlorine, chloramines, and dissolved organic matter — protecting membranes and improving taste profile.
Precision Filter
High-density micron pre-treatment safeguarding downstream membranes.
Multi-stage cartridge filtration at sub-5-micron resolution removes fine particulates that pass through media filters, extending RO membrane service life significantly.
RO Membrane
Core hyper-filtration eliminating dissolved solids, heavy metals, and micro-contaminants.
Semi-permeable polyamide membrane operating at high pressure forces water through nano-scale pores, rejecting 99%+ of total dissolved solids, bacteria, viruses, and heavy metals.
Mineralization Filter
Balanced post-treatment remineralization restoring essential electrolytes.
Re-introduces calcium, magnesium, and bicarbonate ions stripped by RO, adjusting pH to an optimal alkaline range and restoring mineral profile essential for human hydration.
UV Disinfection
Instantaneous electromagnetic microbiological destruction without chemical additives.
Dual 55W UV lamps at 254nm wavelength disrupt bacterial and viral DNA replication loops at a 2m³/hour throughput rate — chemical-free, zero residue, instant-action sterilization.
Ozone Sterilization
Powerful secondary oxidation providing prolonged antimicrobial protection.
5g/hour ozone injection delivers residual antimicrobial activity inside the sealed product bottle, preventing microbial regrowth during transport and extended shelf storage.
Water Purification Tank
Final sealed product storage vessel ready for safe distribution.
Stainless-lined holding tank stores treated output, feeds the automated filling line, and supports real-time output tracking for production logging and quality assurance.
The Complete Containerized Fortress
40ft integrated container system encompasses Water Treatment, Sterilization, Filling, and Bottle Blowing. The unit is climate-controlled and protected, featuring soundproofing, heat insulation, hot-dip galvanized flooring, integrated floor drains, and an internal air conditioning system.